MaxPro Medical
Explore our cutting-edge medical devices engineered for high precision, continuous health tracking, and seamless integration into modern telehealth ecosystems.
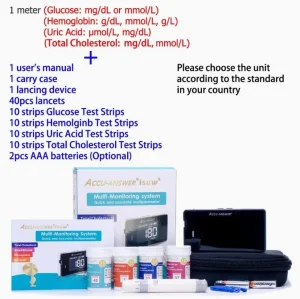
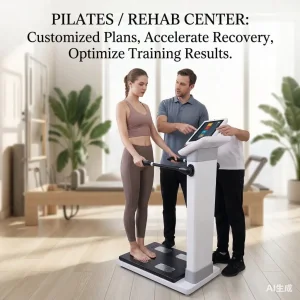
Founded in 2009, Shenzhen MaxPro Medical Co., Ltd. is a leading manufacturer specializing in advanced medical devices and chronic disease monitoring solutions. With a strong commitment to innovation, quality, and customer satisfaction, we provide reliable healthcare technologies to over 500 healthcare institutions and distributors worldwide.
Our company operates a modern 20,000 sq ft manufacturing facility equipped with advanced production and testing systems. Certified under ISO 13485 quality management standards, all of our products comply with international medical regulations, with key products receiving FDA 510(k) clearance and CE certification.
Backed by an experienced R&D team and strict quality control processes, MaxPro Medical continuously develops accurate, user-friendly, and cost-effective medical solutions for chronic disease management, patient monitoring, rehabilitation, and home healthcare applications.
At MaxPro Medical, we uphold the core values of Quality First, Customer Focus, Innovation, Integrity, and Compliance. Our mission is to empower healthcare professionals with dependable medical technologies that improve patient outcomes and enhance healthcare efficiency worldwide.
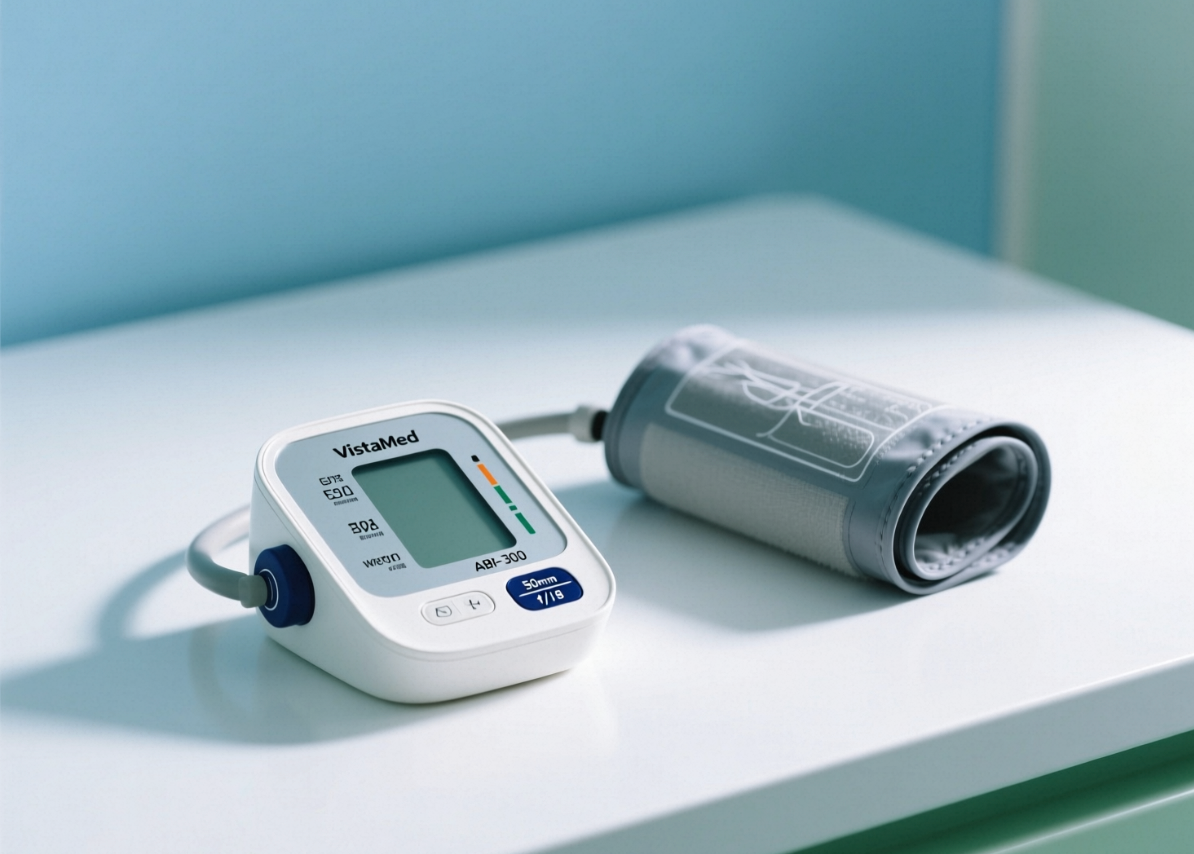
Analyzing market dynamics, procurement shifts, and technological breakthroughs in medication management systems.
As the global population ages and the prevalence of chronic illnesses rises, medication adherence has become a critical challenge for healthcare systems worldwide. Non-adherence accounts for hundreds of billions of dollars in avoidable healthcare costs and millions of hospitalizations annually. Modern smart pill dispensers bridge this gap by integrating IoT connectivity, automated scheduling, biometric security, and real-time cloud alerts. Healthcare providers and institutional buyers are increasingly migrating from traditional pillboxes to automated, programmable dispensing units that synchronize seamlessly with Remote Patient Monitoring (RPM) and Chronic Care Management (CCM) platforms.
International medical distributors, pharmaceutical enterprises, and eldercare facility operators demand high-grade reliability, tamper-proof security, and seamless API integration. Sourcing partners evaluate manufacturers based on strict criteria: traceable component sourcing, robust firmware security, low failure rates, and scalable OEM/ODM capabilities. Shenzhen MaxPro Medical fulfills these stringent expectations by offering turnkey manufacturing solutions tailored to regional regulatory frameworks across North America, Europe, and Asia-Pacific.
Navigating global healthcare markets requires rigorous adherence to local regulations. Our devices are engineered to meet ISO 13485, CE, and FDA 510(k) compliance standards. Furthermore, we offer localized software firmware support, multi-language UI/UX localization, HIPAA-compliant cloud data handling, and regional cellular band compatibility (NB-IoT, 4G LTE-M), ensuring immediate market entry for our global partners.
Looking ahead, the integration of Artificial Intelligence (AI) and Machine Learning (ML) will redefine smart medication management. Future iterations from MaxPro Medical incorporate computer vision for pill verification, predictive analytics to forecast patient adherence drop-offs, and edge-computing voice assistants. Our ongoing R&D investments ensure our B2B partners remain at the absolute forefront of digital health innovation.
With years of experience in the medical device industry, Shenzhen MaxPro Medical Co., Ltd. has built long-term partnerships with healthcare providers, distributors, and medical institutions around the world. Our products are widely recognized for their stable performance, reliable quality, and user-friendly design.
We operate a modern manufacturing facility supported by strict quality management systems to ensure consistent production standards and dependable delivery performance. From raw material sourcing to final product inspection, every process is carefully controlled to meet international medical industry requirements.
MaxPro Medical places strong emphasis on regulatory compliance and product safety. Our manufacturing system is certified under ISO 13485 standards, and selected products have obtained FDA 510(k) clearance and CE certification, ensuring compliance with global market requirements.
Innovation is at the core of our development strategy. Supported by a professional R&D and engineering team, we continuously improve our technologies and provide flexible OEM and ODM solutions tailored to customer needs.
In addition, our dedicated customer service and technical support teams are always ready to provide fast and professional assistance, helping clients achieve efficient and reliable healthcare solutions with confidence.
Precision engineering backed by rigorous multi-stage inspection lines to guarantee flawless medical device production.
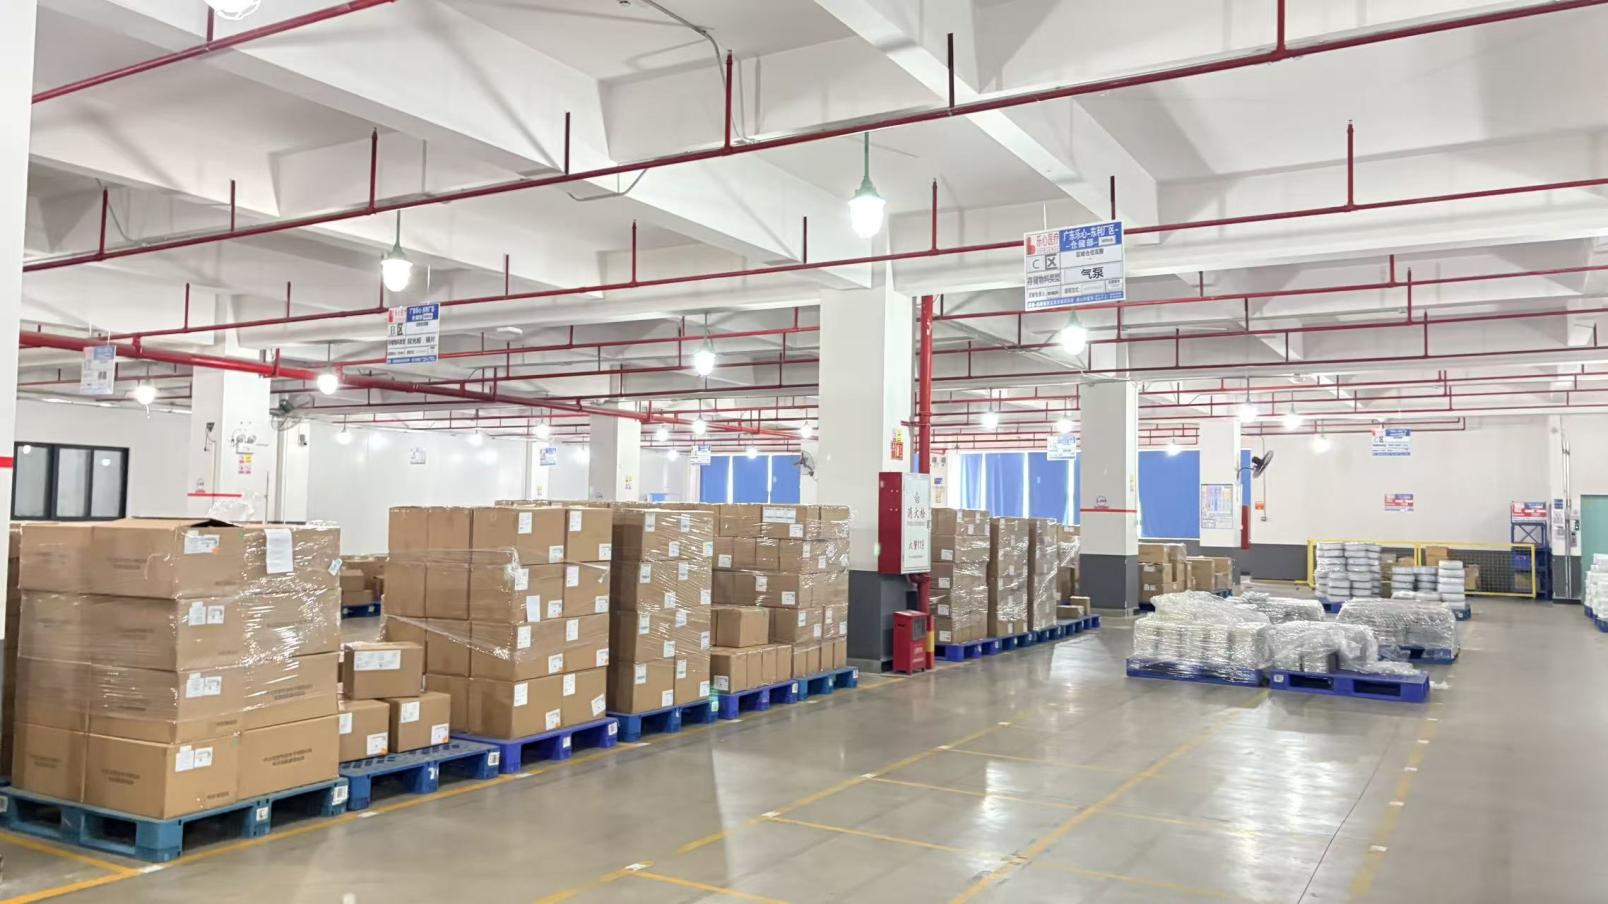
Raw Materials
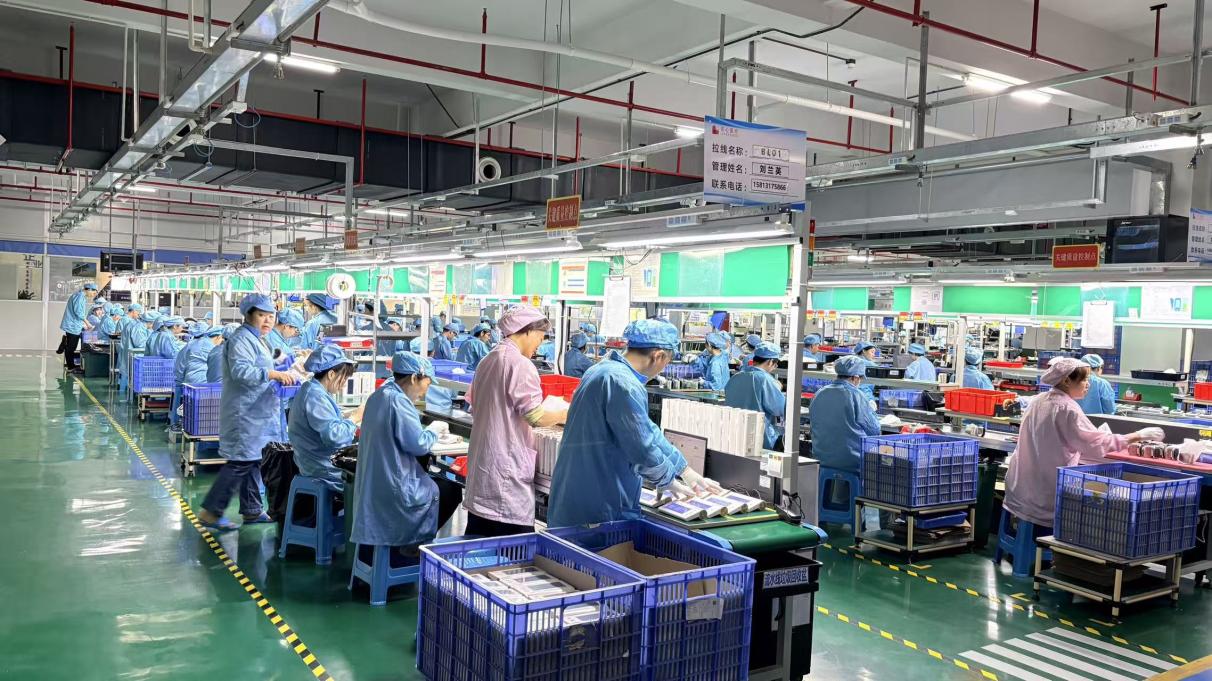
Assembling 1
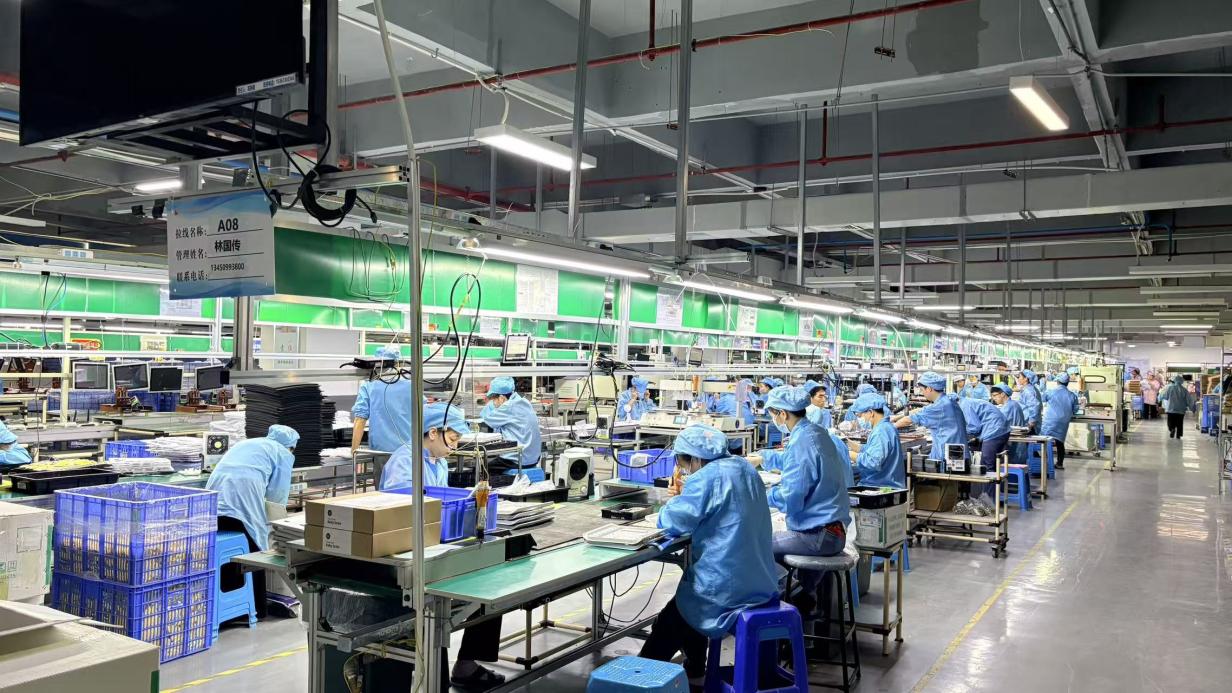
Assembling 2
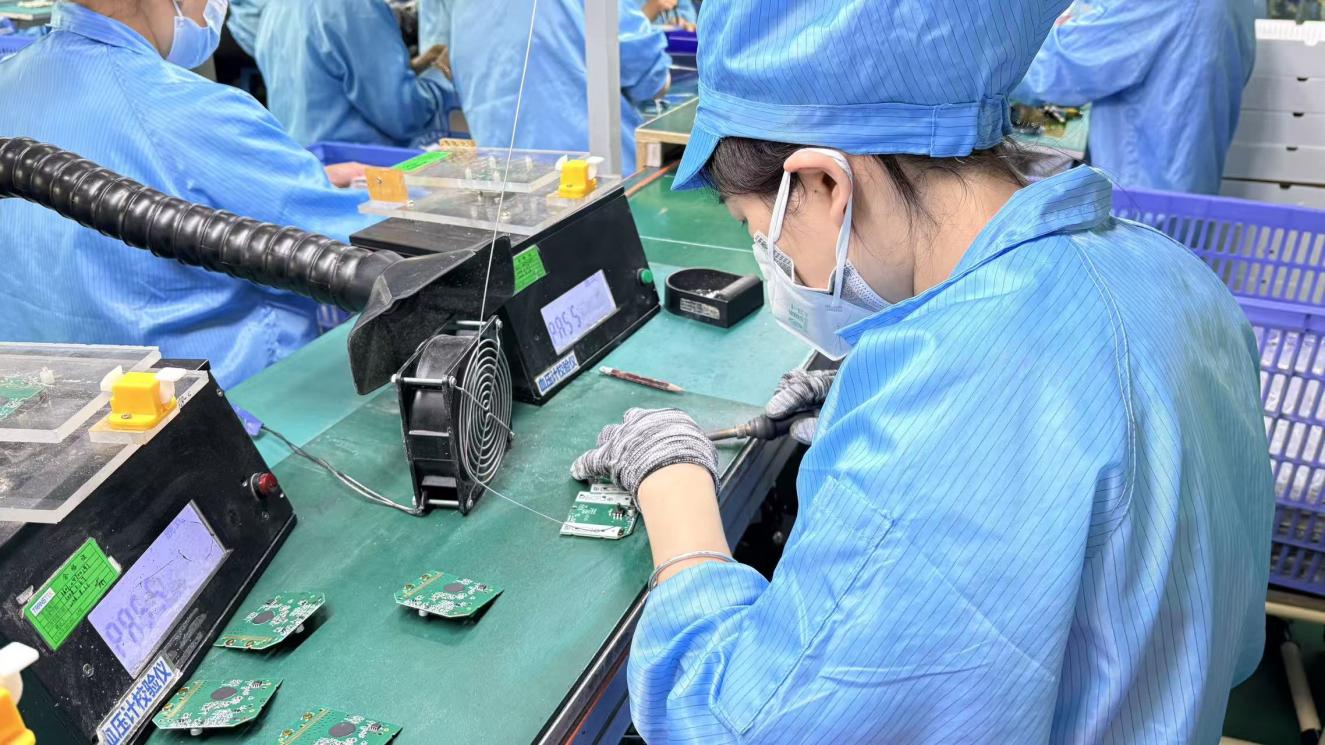
Welding
Inspecting 1
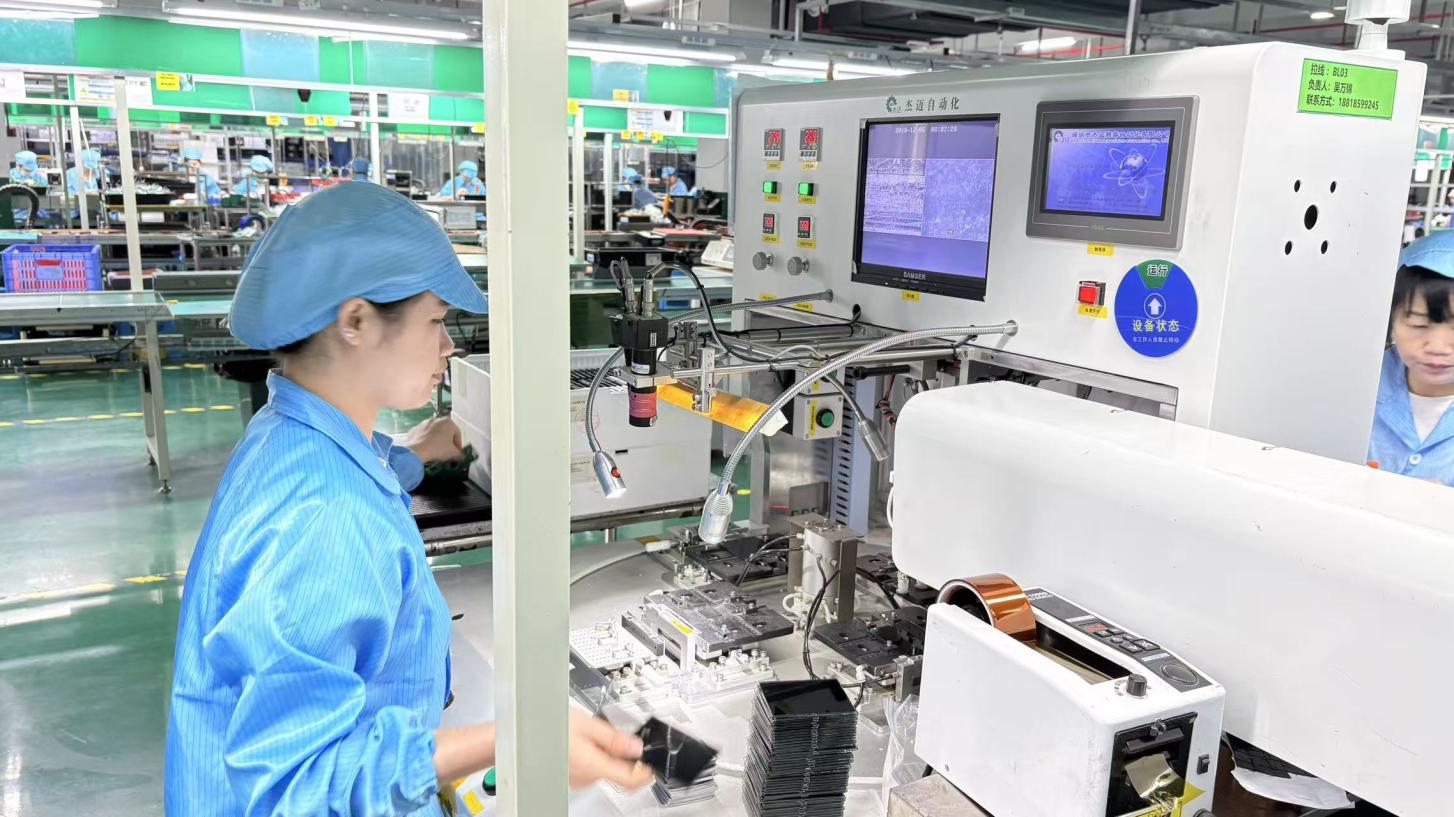
Inspecting 2
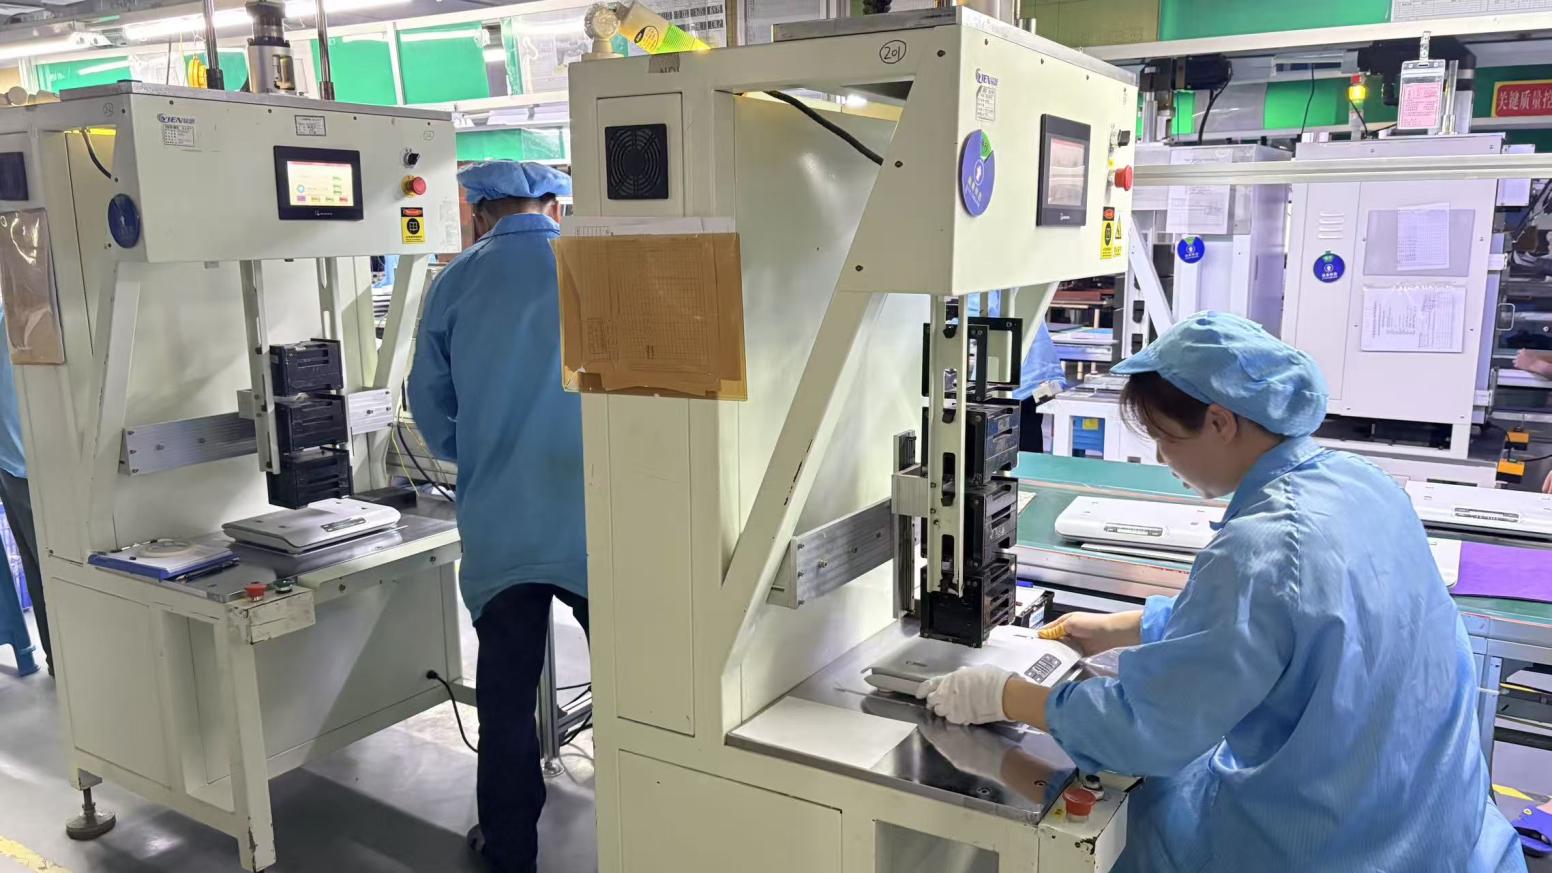
Inspecting 3
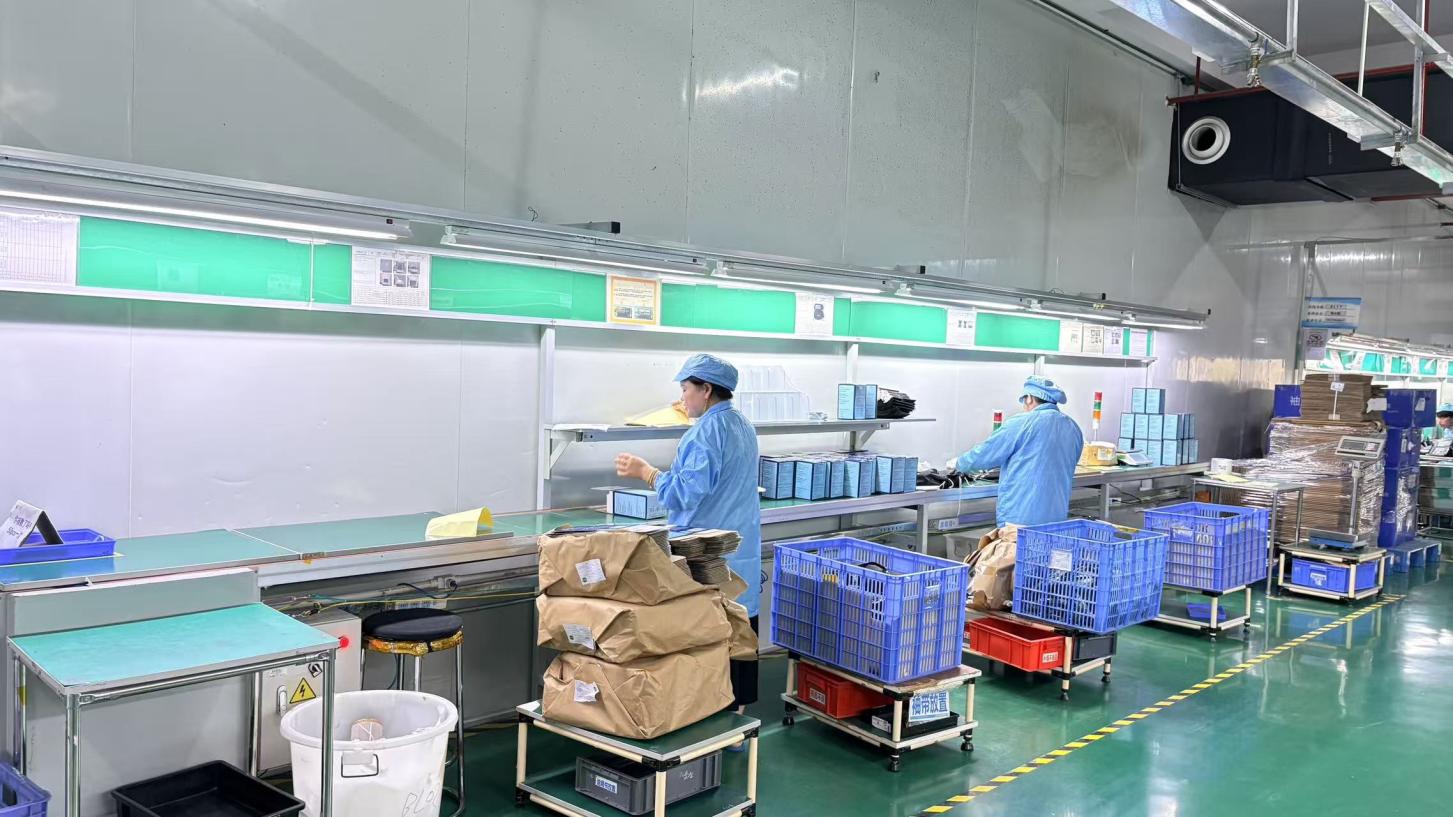
Packing
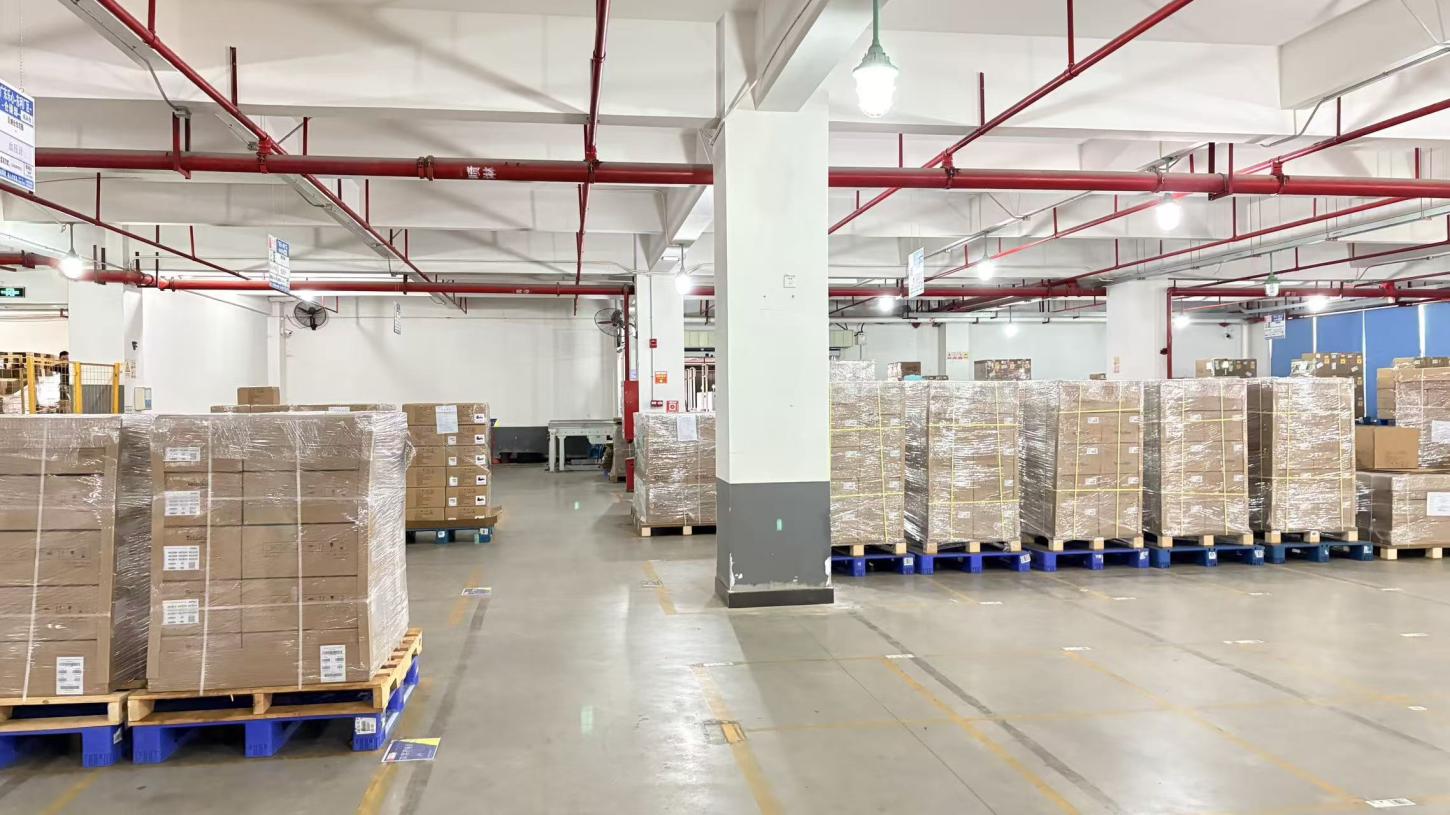
Finished Products
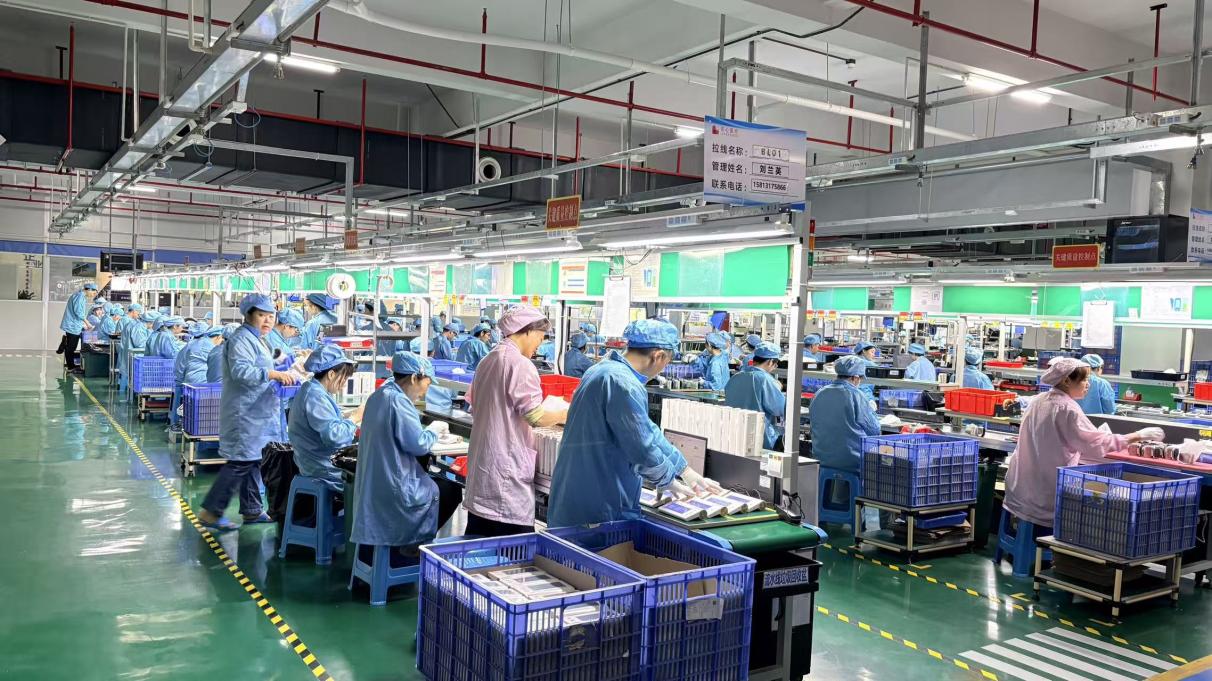
Assembly Line
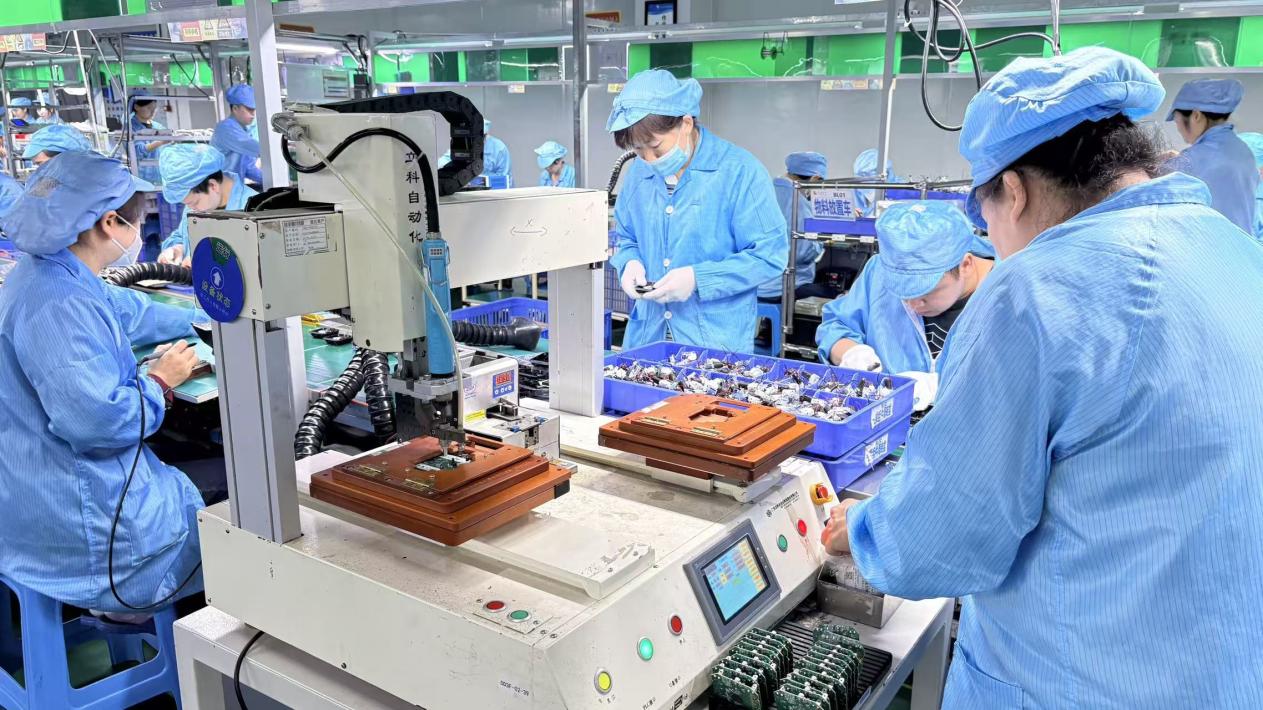
Automatic Screw Driving Machine
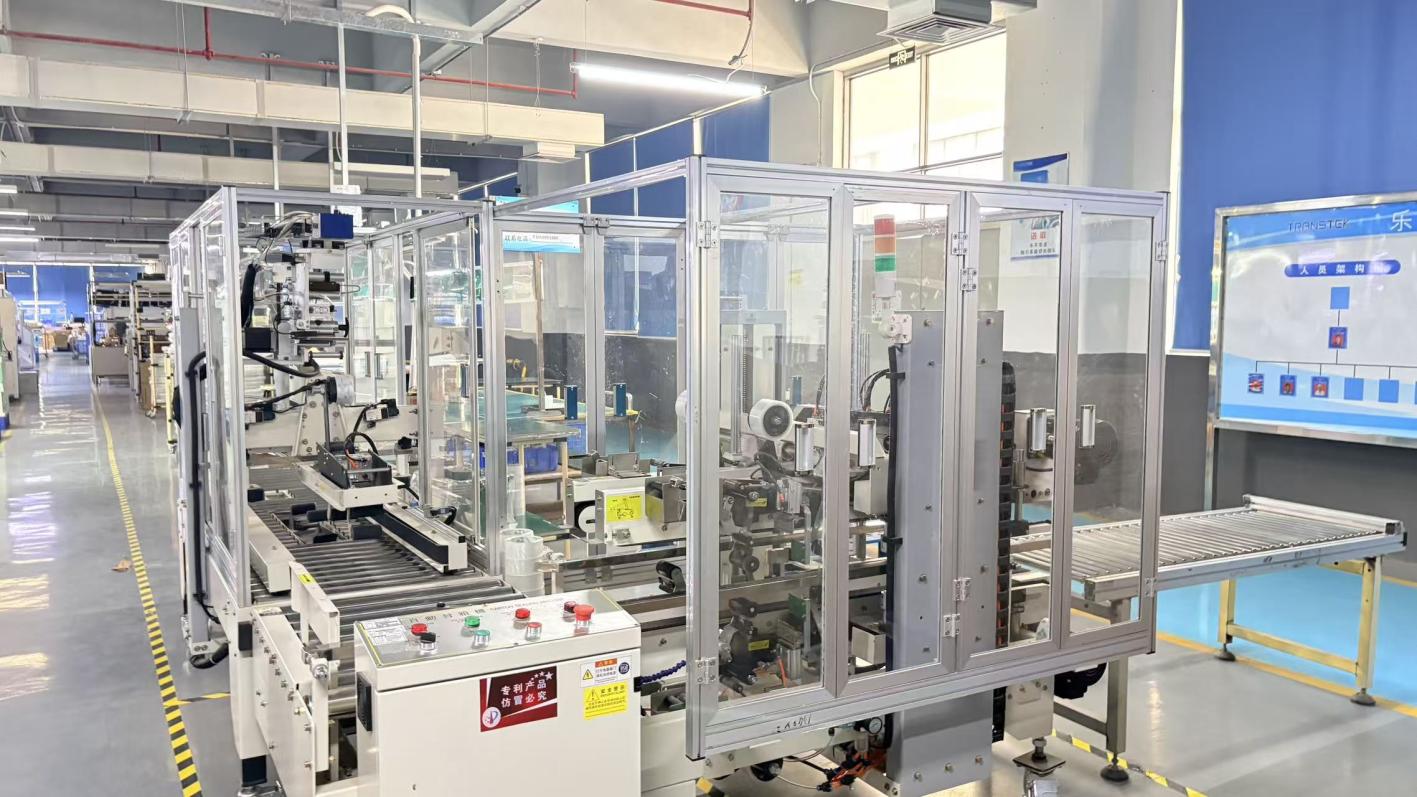
Automatic Packing Line
Expert insights into our manufacturing capabilities, OEM/ODM services, and regulatory compliance.
Our manufacturing facility operates under ISO 13485 quality management standards. Our core product lineup complies with international medical regulations, featuring FDA 510(k) clearances and CE certifications suitable for global distribution.
Yes, we specialize in comprehensive OEM and ODM solutions. Our R&D and engineering teams collaborate closely with clients to tailor hardware design, firmware logic, cloud connectivity, and custom packaging to specific brand and market requirements.
Backed by our automated manufacturing lines and 20,000 sq ft production facility, standard bulk orders are typically fulfilled within 3 to 5 weeks, depending on customization complexity and order volume.
Our connected devices utilize secure cellular (NB-IoT/LTE-M) and Bluetooth protocols along with standardized API integration frameworks, allowing healthcare providers to sync patient compliance data instantly into their existing Remote Patient Monitoring software.
Discover more of our professional-grade medical equipment engineered for precision, reliability, and clinical excellence.